
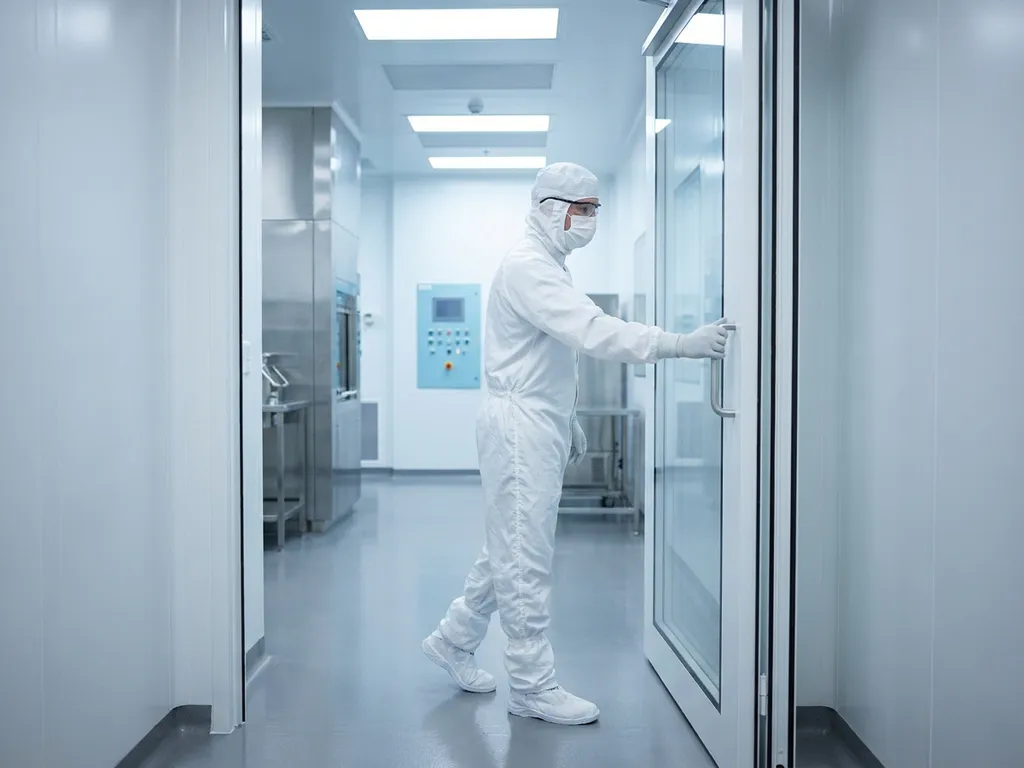
The role of gowning in pharmaceutical manufacturing plays a critical role in pharmaceutical contamination prevention by acting as a physical barrier between personnel and the controlled environment. Human skin, hair, and clothing are among the most significant sources of viable and non-viable particulates in cleanrooms and sterile manufacturing zones.
Effective gowning therefore helps reduce the transfer of human-generated particles and microorganisms, but it should always be considered as one component of a broader contamination control programme rather than a standalone control. The sections below address the most important questions surrounding gowning practices, requirements, and limitations.
What contaminants does gowning actually prevent?
Gowning prevents the transfer of human-generated contaminants into controlled environments. These include skin flakes, hair, respiratory droplets, cosmetic residues, fabric fibres, and microorganisms carried on the body’s surface. In pharmaceutical and medical device settings, both viable contaminants such as bacteria and fungi and non-viable particles such as dust and lint pose serious risks to product integrity.
The human body continuously sheds particles, with estimates from industry literature suggesting that a person at rest generates a significant number of particles per minute, rising sharply with movement. Gowning garments, when correctly selected and worn, intercept these particles before they enter the surrounding air or settle on critical surfaces. Gloves prevent hand contact contamination, hoods contain hair and scalp particles, and face masks reduce the dispersal of respiratory aerosols.
The effectiveness of gowning at capturing these contaminants depends heavily on garment material, fit, and integrity. Woven garments offer limited filtration compared to non-woven or laminated fabrics specifically designed for cleanroom use. The effectiveness of gowning depends on several factors, including garment design, material, fit, integrity, laundering or sterilisation processes where applicable, and correct donning technique.
Tears, loose seams, or improperly sealed interfaces at the wrist and neck can allow contaminants to escape regardless of how carefully the garment is donned. Reusable cleanroom garments should also be managed through an appropriate garment programme that includes qualified laundering, inspection, sterilisation where required, and controls over garment condition and useful life.
What are the standard gowning requirements in GMP environments?
Gowning requirements in GMP environments depend on the manufacturing activity, contamination risk, cleanroom grade, facility contamination control strategy, and applicable regulatory framework.
EU GMP Annex 1 establishes specific gowning expectations for sterile medicinal product manufacturing. FDA guidance also addresses personnel clothing and aseptic practices in sterile manufacturing. The ISO 14644 series supports the operation of cleanrooms and associated controlled environments, but ISO cleanroom classes do not prescribe a universal gowning ensemble for each particle classification.
For Grade A/B aseptic operations, personnel should wear garments designed to minimize shedding and retain particles generated by the body. Annex 1 describes Grade A/B clothing that includes appropriate sterilised garments, head covering, face mask, sterile eye coverings, sterilised gloves, and sterilised footwear or overboots.
Grade C and D areas require clothing appropriate to the activities and contamination risks being controlled. Hair and, where relevant, facial hair should be covered. Gloves should be worn in Grade C and D areas where the activity presents a contamination risk, as defined through the facility’s contamination control strategy, rather than being assumed to be mandatory for every activity.
The specific garment requirements, including materials, construction, cleaning, sterilisation where applicable, and replacement criteria, should be documented within facility procedures. Beyond the garments themselves, GMP environments require appropriately designed changing and gowning areas where personnel transition between areas of different cleanliness.
How does gowning order affect contamination control outcomes?
Gowning order directly affects contamination control outcomes because donning garments in the wrong sequence can transfer contaminants from less clean surfaces to cleaner ones. A standardised, documented gowning sequence ensures that each item is put on without contaminating the next, and that personnel move progressively from the least clean to the most critical garment.
A typical gowning sequence for a high-grade environment begins with hand hygiene, followed by a hood or head covering, then the coverall or gown, overshoes or boot covers, and finally gloves. Face masks are generally applied before the coverall to avoid touching the face after gloving. In aseptic environments, a final glove change or sanitisation step is often required immediately before entering the critical zone.
Deviations from the established sequence, even seemingly minor ones such as putting on gloves before the coverall, create opportunities for contamination transfer. Training programmes should reinforce the rationale behind each step rather than treating gowning as a routine checklist, since understanding the contamination logic behind the sequence encourages more consistent compliance across shifts and personnel.
Understanding these contamination pathways helps personnel perform gowning consistently rather than treating the procedure as a simple checklist.
What is the difference between gowning grades for different cleanroom classifications?
Gowning requirements generally become more stringent as contamination risk and environmental control requirements increase, but they should not be assumed to correspond directly to an ISO particle classification alone.
Under EU GMP Annex 1, different gowning expectations apply across Grades A through D.
For Grade D areas, hair and, where relevant, facial hair should be covered, and appropriate protective clothing and footwear should be worn.For Grade C areas, personnel should wear appropriate cleanroom garments that cover the hair, facial hair where relevant, arms, and legs. Gloves are used where required by the activity and contamination risk.
For Grade A/B aseptic operations, personnel wear sterilised garments intended to retain particles and microorganisms shed by the body, together with appropriate head covering, face mask, sterile eye covering, sterile gloves, and sterilised footwear or overboots. Grade A should also be understood as the critical processing zone rather than simply another personnel gowning level. In many open aseptic processes, Grade A conditions are maintained at the point of critical operation with a Grade B background environment.
The ISO 14644 series uses airborne particle concentration to classify cleanrooms.
ISO Class 5, ISO Class 7, and ISO Class 8 designations therefore describe airborne particle cleanliness, not a prescribed garment set. The facility must determine appropriate gowning based on the process, product risk, operational state, and regulatory requirements. Garment characteristics such as particle retention, low shedding, electrostatic properties, durability, and sterility where required should be selected to support the conditions in which they will be used.
Why does gowning alone not guarantee a contamination-free environment?
Gowning alone does not guarantee a contamination-free environment because it addresses only one of several contamination pathways. Personnel are a significant source of contamination, but equipment, materials, air handling systems, and facility surfaces, particularly floors, also introduce particles and microorganisms into controlled spaces. A comprehensive contamination control strategy must address all of these vectors simultaneously.
Other gaps in gowning-only programmes include human behaviour variability, garment degradation over time, inadequate gowning room design, and insufficient monitoring. Personnel who rush the gowning process, reuse garments beyond their validated lifespan, or fail to follow the correct sequence can undermine even the most carefully written procedure. Environmental monitoring data should be reviewed regularly to identify patterns that suggest gowning or other controls are underperforming.
How should pharmaceutical facilities qualify gowning practices?
For personnel entering aseptic processing environments, documented gowning qualification and periodic requalification are important parts of contamination control. Qualification should demonstrate that personnel can consistently perform the approved gowning procedure without introducing unacceptable levels of contamination.
A gowning qualification programme may include direct observation of technique and microbiological monitoring of defined garment locations and gloves after gowning.Contact plates and glove or fingertip sampling are used to assess microbiological contamination. They should not be described as measurements of “viable particle counts.”
Initial qualification should be completed before personnel are authorized to perform activities within applicable aseptic areas, with periodic requalification used to confirm that acceptable practices continue to be maintained. Training records, gowning observations, personnel monitoring results, and environmental monitoring trends can all contribute to the ongoing assessment of gowning performance.
How Dycem supports floor-level contamination control alongside gowning
While gowning is essential, it cannot address every contamination pathway on its own. Footwear and wheeled equipment can transfer floor-borne particles across entrances and transition points, making floor-level contamination one of the pathways that may need to be addressed within a facility’s wider contamination control strategy. Dycem’s reusable contamination control mats are specifically engineered to capture up to 99.9% of shoe and wheel contaminants at entry points, working alongside gowning protocols to close one of the most significant gaps in facility hygiene compliance.
Dycem’s solutions are designed to integrate directly into the environments where gowning takes place and beyond:
- Dycem CleanZone mats are ideal for gowning rooms, airlocks, and cleanroom entrances, capturing particulates from footwear before personnel enter critical zones
- Dycem WorkZone mats handle heavy-wheeled traffic such as pallet trucks and forklifts, preventing contamination transfer through logistics and material handling routes
- Dycem Floating Mats provide flexible, repositionable protection for facilities with changing layouts or temporary controlled zones
- All Dycem mats are reusable, built with integrated Biomaster antimicrobial protection, and manufactured to ISO 9001 and 14001 standards, making them a sustainable and audit-ready alternative to disposable sticky mats
Dycem’s contamination control specialists offer a free site survey to assess your facility’s entry points, cleanroom classifications, and contamination risk profile. Explore the full range of contamination control mat solutions or contact the Dycem team to arrange a consultation and find out how Dycem can strengthen your facility’s overall hygiene compliance program.
References
- European Commission. EU Guidelines for Good Manufacturing Practice, Annex 1: Manufacture of Sterile Medicinal Products. EudraLex Volume 4, 2022.
- U.S. Food and Drug Administration. Sterile Drug Products Produced by Aseptic Processing, Current Good Manufacturing Practice: Guidance for Industry. September 2004.
- International Organization for Standardization. ISO 14644-1:2015, Cleanrooms and associated controlled environments, Part 1: Classification of air cleanliness by particle concentration.
- International Organization for Standardization. ISO 14644-5:2025, Cleanrooms and associated controlled environments, Part 5: Operations.
- U.S. Food and Drug Administration. 21 CFR Parts 210 and 211, Current Good Manufacturing Practice for Drugs.